que cherchez-vous?
Ordering aluminum heat shield material by square meters alone does not tell the supplier how efficiently it will move through the customer's fabrication process. Sheet dimensions affect blank yield, trimming waste, pattern orientation, forming operations, packaging and ultimately the cost of every finished heat shield.
For an OEM program, the most useful aluminum heat shield sheet size is therefore not necessarily the largest available sheet. It is the size that produces the required blanks with controlled waste and fits the customer's cutting, stamping and handling process.
BSTFLEX supplies embossed aluminum heat shield sheet for automotive exhaust, engine bay, underbody and other thermal protection applications. Standard listed sizes include 300 × 500 mm, 500 × 500 mm and 500 × 700 mm. For OEM requirements outside these formats, provide the required dimensions and production quantity for project review.
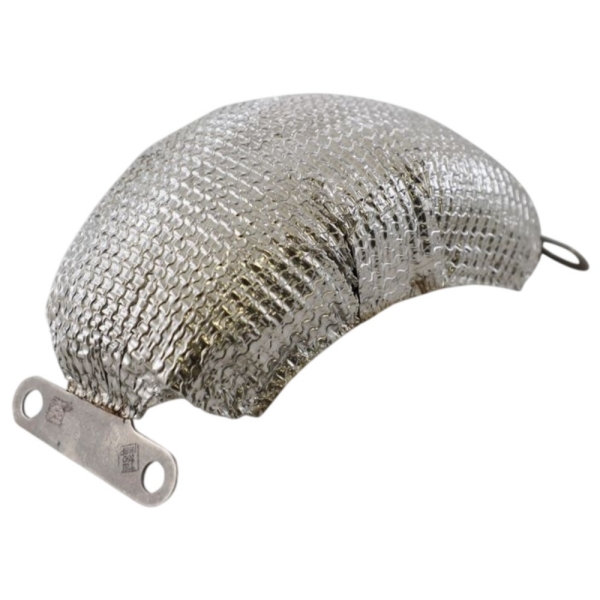
The correct raw material size should be developed backward from the finished component.
A customer manufacturing a flat barrier may need little more than trimming around the perimeter. A three-dimensional automotive heat shield can require additional material for bends, flanges, mounting tabs, formed edges and final trimming.
This means three dimensions should be kept separate:
They are rarely identical.
If a finished shield measures 420 × 280 mm, for example, ordering material in exactly that size may leave no allowance for edge returns, holding areas or final trimming. The blank should first be developed from the forming process, and the purchased sheet should then be selected from the blank layout.
The current BSTFLEX embossed aluminum thermal barrier sheet range lists the following standard panel dimensions:
| Part Number | Sheet Size | Typical Purchasing Use |
|---|---|---|
| AL0305 | 300 × 500 mm | Small shields, prototypes and localized thermal barriers |
| AL0505 | 500 × 500 mm | Medium-size panels and general fabrication work |
| AL0507 | 500 × 700 mm | Larger blanks and applications requiring additional forming or trimming area |
These dimensions provide practical starting points. They should not be interpreted as the only possible OEM requirement. Where production quantities justify a different material format, state the requested size in the RFQ so supply feasibility can be confirmed.
The phrase cut to size aluminum heat shield can refer to several very different supply stages.
A buyer may be asking for:
These should not share the same quotation description.
When sending an inquiry, identify the exact delivery condition required. If only raw sheet is needed, provide sheet dimensions. If the supplier is expected to cut the finished outline, provide a controlled drawing. If forming is also required, supply the finished component drawing in addition to the blank geometry.
A flat blank must contain enough material to create all features in the finished shield.
Typical features affecting blank dimensions include:
For simple folds, fabrication engineers can calculate an initial blank from the bend geometry and then validate it through trial forming. Complex stamped shields normally require blank-development work based on the actual tooling and material behavior.
Do not add an arbitrary percentage to every side of the finished component and treat that as the production blank. Additional material should have a defined purpose.
Some heat shield geometries are easier to control when the part is formed first and trimmed afterward.
In these cases, the initial blank deliberately includes excess material around selected edges. This material provides room for forming variation and can be removed after the part reaches its final three-dimensional shape.
The drawing should distinguish:
Without this distinction, purchasing may compare quotations for two apparently identical sheets even though one supplier has included necessary process material and the other has not.
OEM buyers should evaluate how many usable blanks can be produced from each purchased sheet.
Consider two sheet formats with similar total area. If one allows four blanks to nest efficiently while another produces only three because of pattern direction or edge allowances, the lower price per square meter may not produce the lower cost per heat shield.
A useful material-cost comparison is therefore:
Purchased sheet cost ÷ number of acceptable blanks produced from that sheet
Then add the relevant cutting, trimming and scrap-handling costs.
For repeat programs, send the supplier a nesting drawing where possible. This makes sheet-size discussions much more precise than quoting only the approximate area of the finished part.
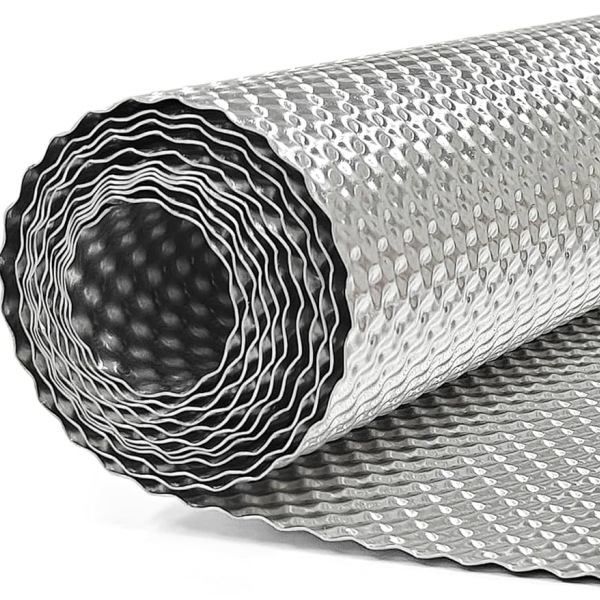
Embossed aluminum heat shield material has a three-dimensional surface rather than a plain flat finish. Depending on the selected pattern and subsequent forming operation, orientation may need to remain consistent from one blank to another.
If orientation is important, show it clearly on the blank drawing.
Useful drawing information can include:
Do not rotate blanks during nesting purely to increase material yield if the approved component requires a controlled orientation.
When discussing aluminum heat shield sheet sizes, thickness needs its own definition.
The thickness of the original aluminum sheet and the overall height of an embossed profile are not necessarily the same measurement. A deeply textured material occupies a larger three-dimensional envelope than the base metal gauge alone suggests.
For an OEM specification, identify exactly which measurement is being controlled.
Typical fields include:
| Specification | What It Describes |
|---|---|
| Base metal thickness | The thickness of the aluminum material itself |
| Embossing profile | The geometry created in the material surface |
| Overall embossed height | The total envelope occupied by the patterned sheet where this measurement is required |
| Finished shield envelope | The overall dimensions of the formed component |
Using the word “thickness” for all four measurements can create purchasing errors.
Prototype workshops often prefer manageable sheets that can be marked, cut and shaped without specialized material-handling equipment.
A smaller standard panel can be useful where only one or two shields need to be evaluated before the production blank has been finalized.
For repeat production using profile cutting or blanking, the priority changes to material utilization and consistent blank orientation.
Sheet dimensions should be matched to the nesting layout and cutting equipment. Large unused borders are a recurring cost, not merely prototype waste.
For a stamped automotive heat shield, the blank dimensions should be developed around the forming process. Material required for drawing, flange formation or final trimming must remain available until the relevant operation is complete.
If the customer requires a finished stamped component rather than raw aluminum sheet, provide the complete drawing and define the supply scope separately.
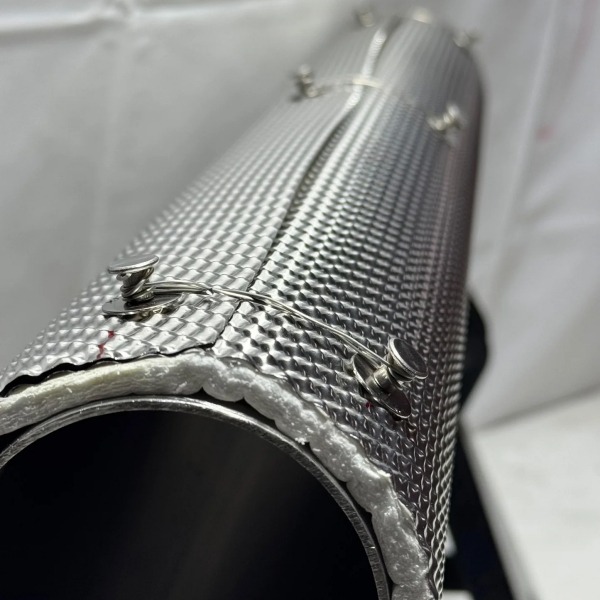
A standard panel is often the most convenient choice for development quantities, service parts and lower-volume fabrication. It provides a known starting format without creating a new material-size requirement.
A project-specific sheet or blank becomes more attractive when:
Custom size availability should be confirmed during quotation for the requested alloy, temper, pattern, thickness and quantity. Do not assume that every possible dimension can be produced from every material combination.
Buying blanks instead of full sheets can reduce internal cutting work when the component geometry and production process are already stable.
This approach can make sense for:
However, a blank only adds value when its geometry is controlled.
The purchasing drawing should identify dimensions, tolerances, datums, corner radii, holes if included, pattern orientation and edge requirements.
BSTFLEX supplies aluminum heat shield material, but some projects require a completed metal heat shield rather than sheet stock.
Keep these inquiries separate.
Material inquiry: alloy, temper, base-metal thickness, pattern, sheet dimensions, quantity and packaging.
Blank inquiry: all material details plus blank drawing, profile tolerances and edge requirements.
Finished heat shield inquiry: complete component drawing, forming geometry, holes, mounting details, interfaces and validation requirements.
For formed metal components, customers can also review the BSTFLEX metal stamping heat shield range.
Packaging should protect more than the visible surface.
Thin embossed panels can be damaged by uncontrolled handling, crushed edges or heavy items placed on top of the pack. Define the pack according to the dimensions and the customer's receiving process.
For an OEM order, useful packaging information includes:
Packaging requirements should be agreed for the actual product. A suitable pack for a 300 × 500 mm sheet may not be appropriate for a much larger custom panel.
A precise inquiry allows quotations to be compared on the same basis.
| RFQ Field | Information to Provide |
|---|---|
| Application | Exhaust, engine bay, underbody, fuel tank, firewall, transmission tunnel or other location |
| Alloy | Required aluminum alloy or state that supplier review is requested |
| Temper | Specified material condition where applicable |
| Base-metal thickness | Required nominal gauge and tolerance if controlled |
| Embossing pattern | Existing pattern reference, drawing or approved sample |
| Supply format | Standard sheet, custom rectangular sheet, blank or formed component |
| Dimensions | Required length and width, including whether these refer to sheet or finished blank |
| Pattern orientation | State whether orientation must remain controlled |
| Quantity | Prototype requirement, normal batch quantity and annual forecast |
| Packaging | Pack quantity, identification and protection requirements |
The current BSTFLEX product range lists 300 × 500 mm, 500 × 500 mm and 500 × 700 mm embossed aluminum heat shield sheets. For an OEM project requiring another format, provide the requested dimensions and quantity so availability can be reviewed.
Yes. The material is designed to be cut, folded and shaped for thermal barrier fabrication. For repeat production, define whether the requirement is a rectangular sheet, flat blank or finished formed component because each requires different purchasing information.
Not necessarily. Forming, folded edges, mounting tabs and final trimming can require a larger starting blank. Develop the flat blank from the finished geometry before selecting the purchased sheet size.
A blank is the flat piece of material prepared for subsequent forming or assembly. It can be rectangular or profile-cut depending on the manufacturing process. Its dimensions should be controlled separately from the finished heat shield dimensions.
No. Purchasing efficiency depends on usable blank yield, cutting waste, pattern orientation, handling and the customer's fabrication process. Compare cost per acceptable blank rather than sheet area alone.
Yes, where their geometry, pattern orientation and fabrication requirements allow it. A nesting layout can improve material utilization in repeat OEM production.
BSTFLEX supports OEM thermal protection projects and metal heat shield fabrication. Finished-part requirements should be quoted from drawings or samples so material, forming, cutting and inspection scope can be defined correctly.
For a standard panel, review the current BSTFLEX Embossed Aluminum Thermal Barrier Sheet sizes and identify the format that fits your prototype or fabrication requirement.
For production projects, send the flat blank and finished-part drawing where available. Include alloy, temper, base-metal thickness, embossed pattern, required dimensions, prototype quantity and expected production volume.
If aluminum is not suitable for the thermal or mechanical requirements of the installation, BSTFLEX also supplies embossed stainless steel heat shield material and Alloy 625 Inconel heat shield material for other operating conditions.
Send your aluminum heat shield sheet dimensions and RFQ to BSTFLEX for material, size, sample and OEM production review.
Mots clés :
No.10, Chuangxin North Road, Nanshan Park, Ningguo Economic and Technological Development Zone, Ningguo City, Anhui Province, China
tél/Whatsapp : 0086-15856303740
e-mail : sales@bstbraidedsleeve.com
Skype : vanesa-cheng